IQ, OQ, PQ: qualifying a press and a mould before producing for pharma
A new mould has just been fitted to its press. The first parts look good. For medicine packaging, that is not enough: you must prove, with documents, that the set-up is properly installed, that it works within its limits and that it produces correctly, again and again.
By Tecmom editorial team · 2 min read
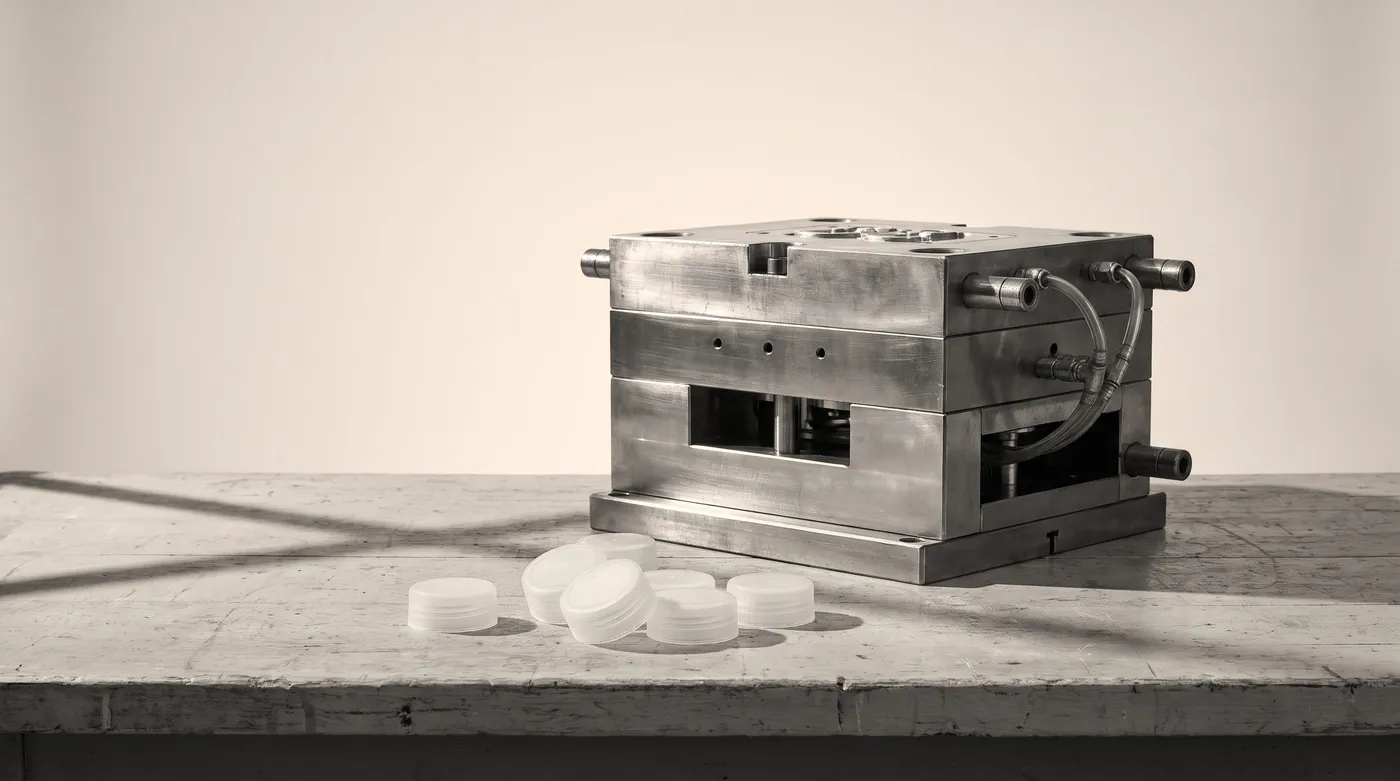
A logic drawn from good practice
European good manufacturing practice (GMP) devotes its Annex 15 to the qualification of equipment and the validation of processes. In the version applicable since 1 October 2015, it describes a series of steps, each documented, starting from a user requirements specification.
These rules are aimed first at medicine manufacturers. The GMP applied to packaging by ISO 15378 follows the same logic for primary packaging materials.
IQ: is it properly installed?
Installation qualification (IQ) verifies that the equipment, as installed, complies with its design and the manufacturer's recommendations. Annex 15 includes checking components and connections against the drawings, collecting the supplier's instructions, calibrating instruments and verifying materials of construction.
For a press and a mould, this means for example the cooling circuits, the temperature and pressure sensors, the material dryers.
OQ: does it work within its limits?
Operational qualification (OQ) verifies that the equipment works as intended across its whole operating range. It includes tests at the upper and lower limits, or under worst-case conditions.
In injection moulding, temperatures, pressures and times are varied up to the edges of the process window, and parts are checked to remain compliant. Once OQ is complete, operating procedures, training and preventive maintenance can be finalised.
PQ: does it produce right, repeatedly?
Performance qualification (PQ) verifies that the equipment performs effectively and reproducibly with the approved process and specifications. It is carried out with production material, under normal conditions, on representative runs.
The parts are then measured and inspected; monitoring continues afterwards through statistical process control. Finally, Annex 15 requires equipment to be re-evaluated at an appropriate frequency, and requalified after any significant change: see change control.
IQ, OQ, PQ: three acronyms for a single idea. A compliant part proves nothing unless you can show it will still be compliant tomorrow.
Glossary
- Qualification
- Documented proof that equipment is fit for its use.
- Validation
- Documented proof that a process reproducibly delivers a compliant result.
- IQ, OQ, PQ
- Installation, operational and performance qualification.
- Process window
- The range of process settings within which parts remain compliant.