Extrusion or injection blow moulding: two ways to make a bottle
A plastic bottle is always inflated like a balloon inside a mould. What matters is what gets inflated: a plain tube of melt, or a blank whose neck is already finished. That choice decides how precise the neck is, and therefore how well the bottle seals.
By Tecmom editorial team · 3 min read
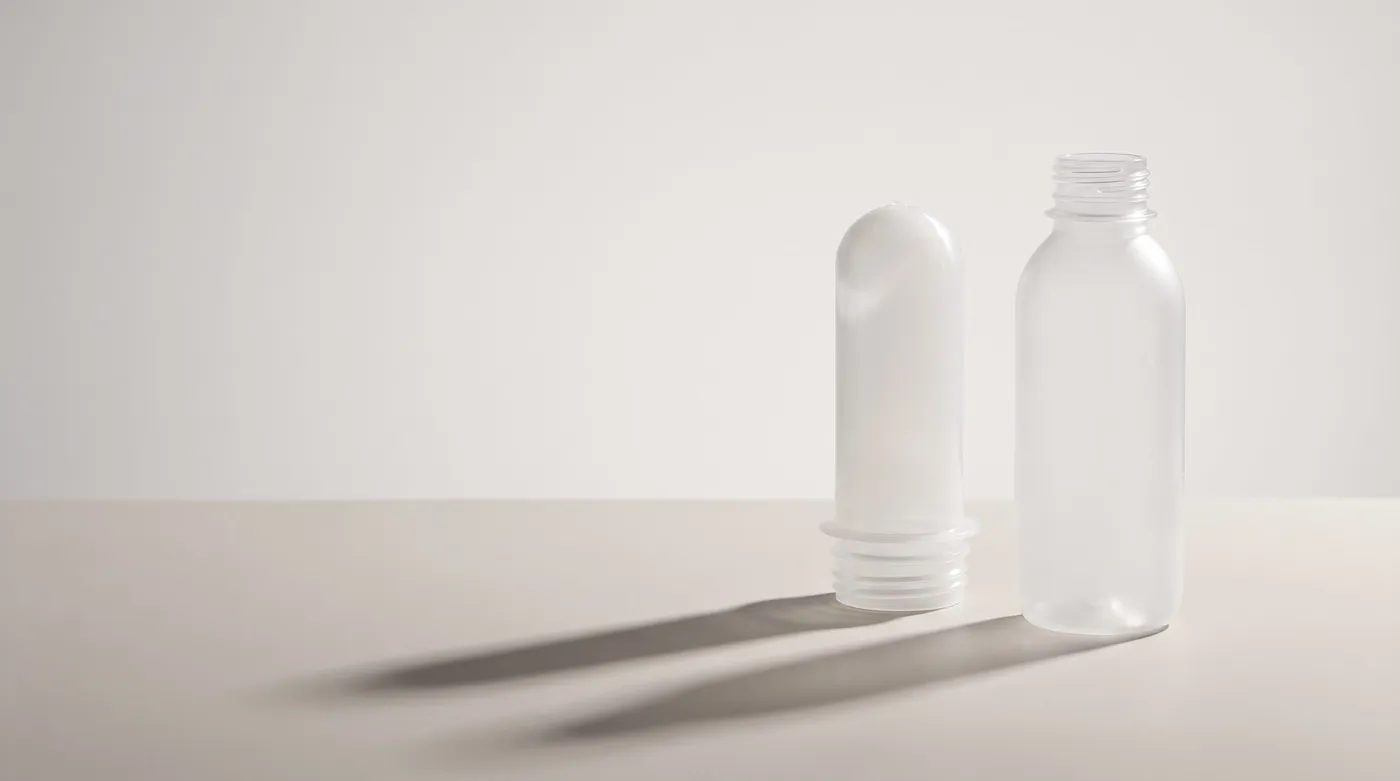
Inflating, either way
Blow moulding makes hollow bodies: bottles, flasks, cans. A blank of softened plastic is enclosed in a mould, then compressed air presses it against the walls, where it cools and takes shape. Two main families of processes differ in the nature of that blank and in how it is made.
Extrusion blow moulding: a tube that gets pinched
In extrusion blow moulding, an extruder continuously pushes out a tube of molten material, the parison. The mould closes on it, pinches it at top and bottom, and air inflates it. The pinched excess, the flash, is then trimmed off; the British Plastics Federation notes that it is usually reground and fed back into the process.
The process has real strengths: lower entry cost for tooling, large volumes, irregular shapes, hollow handles. It is the usual process for jerrycans and large containers. Its limit lies at the neck: it is formed in the parison during blowing, rather than injected to size as in the next process.
Injection blow moulding: the neck is finished first
Injection blow moulding works in two steps. The material is first injected around a core rod, in a first mould, to form a preform: a thick blank that already carries the final neck and thread. While still hot, the preform moves to a second mould where air gives it its shape.
The neck itself is never blown. Its dimensions stay those of the injection. The body comes out with no pinch line and no scrap. Industry sources assign it to small, precise containers, notably for medical use.
What it means for a medicine
A medicine bottle is only as good as its closure. The cap is moulded separately, on another machine; yet it must close tightly, at the first turn as at the thirtieth. The neck finish, the neck and its thread, makes that possible. An injected neck gives that precision from the start.
That is why injection blow moulding is one of the processes Tecmom runs, alongside injection moulding and multilayer extrusion, and why the company designs its own moulds. See our expertise.
Choosing, or rather matching
The choice is not made on part price alone. It depends on the container volume, the precision required at the neck, the quantity needed to pay off the tooling, and the shape wanted. A buyer first chooses a geometry and a quantity; the process tells whether the two are compatible.
Both processes inflate plastic inside a mould. But one trims what it has pinched, while the other finishes the neck before blowing. For a bottle that must close tightly, that difference is the first specification of all.
Glossary
- Parison
- An extruded tube of molten material that is pinched and then blown in extrusion blow moulding.
- Preform
- An injected blank carrying the final neck, blown afterwards in injection blow moulding.
- Flash
- Excess material pinched by the mould and trimmed after blowing.
- Neck finish
- The bottle neck and its thread, designated by their nominal diameter.